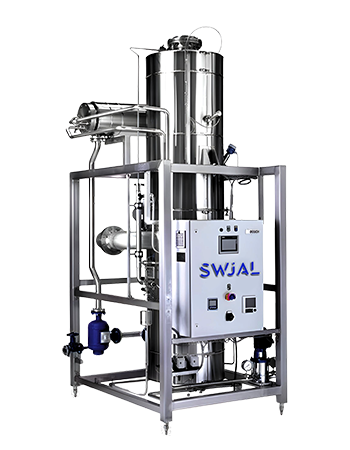
Thursday, March 20, 2025

Pharmaceutical Water Solution: Ensuring High-Purity Water for Pharmaceutical Excellence

 Water is a vital component in pharmaceutical manufacturing, playing a critical role in ensuring product quality, patient safety, and regulatory compliance. Pharmaceutical water solutions are designed to produce high-purity water, meeting stringent global standards set by regulatory bodies like the United States Pharmacopeia (USP), the European Pharmacopoeia (EP), and the Indian Pharmacopoeia (IP). The implementation of advanced water treatment plants has become indispensable for achieving these standards while balancing cost and operational efficiency.

Compliance with Regulatory Standards

In the pharmaceutical industry, water quality is strictly regulated. Depending on its intended use, water must meet specific standards to ensure it does not compromise product safety or efficacy. Key types of pharmaceutical-grade water include Purified Water (PW), Water for Injection (WFI), and Highly Purified Water (HPW). Each type has its own set of guidelines, governing aspects such as microbial content, endotoxin levels, and conductivity.

Regulatory authorities mandate routine monitoring and validation of water treatment systems to guarantee consistent water quality. Compliance requires comprehensive documentation, regular system audits, and the implementation of robust quality control measures. Failure to adhere to these standards can result in regulatory actions, product recalls, and reputational damage, making compliance a top priority.

Cost Considerations in Pharmaceutical Water Solutions

Investing in pharmaceutical water treatment plants involves significant initial costs. However, adopting efficient systems can offer long-term savings. Modern technologies like Reverse Osmosis (RO) and Electrodeionization (EDI) reduce operational costs by minimizing energy consumption and maintenance requirements.

Cost considerations also extend to system scalability, automation, and lifecycle management. Pharmaceutical companies benefit from designing systems that optimize water usage, reduce waste, and integrate seamlessly with existing infrastructure. Selecting high-quality components ensures durability and minimizes downtime, translating into a cost-effective solution over time.

Applications in Pharmaceutical Manufacturing

Pharmaceutical-grade water is used across various stages of production, from raw material processing to final product formulation. Some of the primary applications include:

  • Formulation of Injectable Solutions: WFI is the gold standard for preparing intravenous drugs and vaccines.

  • Cleaning and Sterilization: High-purity water is used to clean equipment and production areas to prevent cross-contamination.

  • Analytical and Laboratory Processes: Consistent water quality is essential for accurate laboratory testing and quality control.

The versatility of pharmaceutical-grade water makes it indispensable in ensuring product consistency and safety throughout the manufacturing process.

Types of Water Treatment Plants for High-Purity Water

Several advanced water treatment technologies are employed to achieve pharmaceutical-grade water:

  • Reverse Osmosis (RO): RO systems use semi-permeable membranes to remove dissolved salts, organic matter, and microbial contaminants. This technology serves as a primary step in producing high-purity water.

  • Electrodeionization (EDI): EDI systems continuously remove ionized species from water, enhancing purity without the need for chemical regeneration.

  • Water for Injection (WFI) Systems: WFI systems produce water of the highest purity, typically using multi-effect distillation or vapor compression. These systems are critical for manufacturing injectables and other sterile pharmaceutical products.

  • Ultrafiltration Systems: Ultrafiltration effectively removes endotoxins and high-molecular-weight contaminants, ensuring water purity meets stringent pharmaceutical standards.

Implementing a combination of these technologies ensures the production of high-purity water, addressing diverse pharmaceutical needs while maintaining regulatory compliance.

Importance of Maintaining Water Quality

Consistent water quality is fundamental to pharmaceutical manufacturing. Contaminants in water can compromise drug formulations, posing risks to patient safety and product efficacy. Regular monitoring, periodic system validation, and preventive maintenance play crucial roles in ensuring system performance and water quality.

Automated systems equipped with real-time monitoring capabilities provide an added layer of assurance, enabling swift corrective actions when parameters deviate from set standards. By investing in comprehensive water treatment solutions, pharmaceutical companies not only meet compliance requirements but also enhance operational efficiency and product reliability.

Conclusion

High-purity water is the backbone of pharmaceutical manufacturing, necessitating advanced water treatment systems to meet strict regulatory standards and ensure product safety. Solutions like Reverse Osmosis, Electrodeionization, and Water for Injection systems are indispensable in achieving the desired water quality. Careful consideration of compliance, cost, and application is crucial for pharmaceutical companies aiming to optimize their processes.

Swjal Process Pvt. Ltd. stands at the forefront of delivering cutting-edge Water for Injection systems, offering unparalleled expertise and innovation in pharmaceutical water solutions. As a leading Water for Injection plant manufacturer in India, Swjal Process Pvt. Ltd. continues to empower pharmaceutical industries with high-purity water systems, ensuring safety, efficiency, and compliance in every drop.

Tuesday, March 11, 2025

WFI Production Methods: Distillation vs. Reverse Osmosis – Which is Better?

 Pharmaceutical manufacturers must choose between distillation and reverse osmosis (RO) for WFI production. Both methods are effective but differ in efficiency, cost, and compliance requirements. Understanding their advantages and limitations helps in selecting the best option.

Distillation vs. Reverse Osmosis

  • Distillation: A traditional method that removes endotoxins, microbes, and dissolved solids through high-temperature vaporization. It ensures high purity but consumes significant energy.

  • Reverse Osmosis (RO) + UF: A modern, energy-efficient alternative that removes contaminants through membrane filtration. However, it requires additional validation to ensure microbial control.

Pros and Cons of Each Method

MethodProsCons
DistillationHighest purity, removes endotoxinsHigh energy consumption, costly maintenance
RO + UFLower energy use, cost-effectiveRequires additional microbial control, more monitoring

Which Method to Choose?

  1. For Large-Scale Plants: Distillation is preferred due to its long-proven effectiveness in pharmaceutical WFI production.

  2. For Energy Efficiency: RO + UF offers lower energy consumption but requires rigorous validation and monitoring.

  3. Regulatory Considerations: USP and EP allow both methods, but compliance depends on proper system design and maintenance.

  4. Cost Factors: While distillation has higher operational costs, RO + UF systems may require frequent membrane replacement and maintenance.

Conclusion

Both methods ensure compliance when properly validated. The choice depends on production scale, cost considerations, and regulatory approvals. Manufacturers must weigh energy efficiency against operational reliability to select the best WFI production method. Understanding these factors helps pharmaceutical companies optimize their water purification processes while maintaining high product quality.


How to Choose the Best Water for Injection Plant for Your Pharmaceutical Needs

 Selecting the right Water for Injection (WFI) plant is crucial for maintaining quality and regulatory compliance in pharmaceutical manufacturing. Factors such as purification methods, energy efficiency, scalability, and compliance play a key role in ensuring reliable production.

Key Factors to Consider

  1. Regulatory Compliance: Ensure the plant meets international standards, such as USP, EP, and WHO guidelines.

  2. Purification Method: Choose between distillation or Reverse Osmosis (RO) + Ultrafiltration (UF), depending on cost, efficiency, and compliance requirements.

  3. Scalability: Opt for a system that can expand to meet future production needs.

  4. Automation & Monitoring: Advanced digital tracking, real-time monitoring, and automated alarms improve quality control and reduce contamination risks.

  5. Energy Efficiency: A plant with sustainable energy use and heat recovery systems helps reduce operational costs.

  6. Maintenance & Support: Choose a manufacturer that provides ongoing technical support, spare parts, and regular maintenance.

Benefits of Investing in the Right WFI Plant

  • Enhanced Product Safety: Eliminates contamination risks, ensuring pharmaceutical quality.

  • Regulatory Compliance: Meets global safety standards, avoiding legal and operational issues.

  • Cost Savings: Improves efficiency, reduces water wastage, and minimizes operational costs.

  • Long-Term Reliability: Ensures sustainable and scalable operations to support business growth.

Conclusion

Investing in the right WFI plant improves efficiency, reduces risks, and ensures regulatory approval. Pharmaceutical companies should assess purification technology, compliance, and scalability before choosing a manufacturing plant. A well-optimized system ensures long-term success and product safety.

Understanding Water for Injection (WFI): Importance and Industry Applications

 Water for Injection (WFI) is a critical component in the pharmaceutical and biotechnology industries. It is used in the production of sterile medications, including injectable drugs, vaccines, and intravenous (IV) solutions. Due to its stringent purity requirements, WFI must be free from contaminants such as bacteria, endotoxins, and particulates. Ensuring high-quality WFI is crucial for drug safety, efficacy, and regulatory compliance.

Importance of WFI

WFI plays a significant role in several pharmaceutical applications:

  1. Pharmaceutical Manufacturing: Used in sterile injectables, biologics, and other parenteral drugs to maintain product safety.

  2. Biotechnology: Supports research applications, including cell culture, protein synthesis, and DNA/RNA-based treatments.

  3. Medical Applications: Found in IV solutions, dialysis treatments, ophthalmic products, and wound irrigation solutions.

  4. Sterilization Processes: Used in cleaning and rinsing sterile equipment, ensuring compliance with good manufacturing practices (GMP).

Industry Applications

The use of WFI extends to:

  • Sterile Drug Manufacturing: Guarantees contamination-free injectable formulations.

  • Medical Device Production: Ensures sterility in surgical and diagnostic instruments.

  • Research and Development: Supports laboratory applications requiring high-purity water.

Conclusion

Water for Injection is a crucial resource in pharmaceutical production, ensuring compliance with USP, EP, and WHO standards. High-quality WFI enhances drug safety and helps pharmaceutical manufacturers meet global regulatory requirements.

Friday, March 7, 2025

Sustainable Water Treatment Solutions for Pharma and Biotech Facilities

The pharmaceutical and biotech industries require large volumes of high-purity water for drug manufacturing, laboratory testing, and bioprocessing. However, traditional water purification methods often consume excessive energy and generate significant wastewater. As environmental sustainability gains priority, companies are adopting eco-friendly water treatment solutions to reduce their carbon footprint while maintaining compliance with regulatory standards.

Water Treatment Solutions for Pharma and Biotech Facilities

Challenges in Traditional Water Treatment

Conventional water purification systems rely heavily on chemical treatments, high energy consumption, and water wastage. Reverse osmosis (RO) systems, while highly effective, can result in significant water rejection, leading to resource inefficiencies. Additionally, thermal distillation for Water for Injection (WFI) consumes substantial amounts of energy, increasing operational costs and environmental impact.

Eco-Friendly Water Purification Technologies

Advancements in water treatment technologies are enabling pharmaceutical and biotech companies to achieve sustainability goals without compromising water quality. Heat-sanitizable RO systems reduce the need for chemical disinfectants while maintaining microbial control. Electrodeionization (EDI) eliminates the use of regeneration chemicals, providing a continuous and environmentally friendly purification process. Membrane-based ultrafiltration and UV disinfection systems offer chemical-free alternatives for microbial control, further reducing environmental impact.

Water Recycling and Waste Reduction Strategies

Water conservation initiatives play a crucial role in sustainable water management. Many pharmaceutical and biotech companies are implementing water recycling and reuse strategies to minimize waste. Reject water from RO systems can be treated and repurposed for non-critical applications such as cooling and cleaning. Zero Liquid Discharge (ZLD) technologies are also being adopted to ensure that all wastewater is treated and reused, preventing environmental pollution.

Regulatory Compliance and Sustainability

Despite the shift towards sustainability, regulatory compliance remains a top priority. The United States Pharmacopeia (USP) and European Pharmacopeia (EP) set strict water quality standards that must be met. Companies must ensure that sustainable water treatment solutions align with these regulations while reducing energy consumption and waste generation.

The Future of Sustainable Water Treatment

With increasing pressure to adopt greener practices, pharmaceutical and biotech companies are exploring innovative solutions such as AI-driven water management, energy-efficient purification systems, and real-time monitoring for predictive maintenance. These advancements not only enhance sustainability but also improve overall operational efficiency and cost-effectiveness.

Conclusion

Sustainable water treatment solutions are revolutionizing the pharmaceutical and biotech industries, offering a balance between environmental responsibility and regulatory compliance. By implementing energy-efficient purification technologies, water recycling strategies, and AI-driven monitoring, companies can significantly reduce their environmental impact while maintaining high-purity water standards. Partnering with us ensuring long-term sustainability and operational efficiency.

Monday, February 24, 2025

Pure Steam Generator Plants

 Pure Steam Generator (PSG) systems are essential for industries requiring high-purity steam for sterilization, including pharmaceuticals, biotechnology, food processing, and healthcare. These systems ensure compliance with cGMP, USP, and FDA standards, delivering contamination-free steam for critical applications.

The demand for pure steam generation has significantly increased as industries recognize the importance of contamination-free environments. Pure steam generators ensure that sterilization processes remain effective by eliminating the risk of microbial contamination. The systems are specifically designed to provide steam with no entrained moisture, endotoxins, or non-condensable gases, making them ideal for sensitive industrial applications. As regulations around steam sterilization continue to evolve, PSG technology is becoming a standard requirement rather than an optional investment.


Pure Steam Generator Plants

Working Principle of a Pure Steam Generator

A Pure Steam Generator operates by converting pre-treated feedwater into pure steam through a controlled heating and separation process. The steps include:

  1. Pre-treatment of Water – Demineralized or distilled water is used to prevent contaminants.

  2. Heating Process – The water is heated using electrically powered or boiler-supplied energy sources.

  3. Separation and Purification – The generated steam passes through separators and demisters, eliminating particulates, ensuring high-purity output.

Proper design and operation of a PSG system are crucial for maintaining consistent steam quality. Any deviation in water quality or temperature control can lead to inefficiencies in the steam production process. Advanced PSG systems incorporate automation and real-time monitoring to regulate steam purity, ensuring continuous compliance with international standards. The ability to produce pure steam on demand without fluctuations in quality makes these systems an essential investment for industries that require precise sterilization.

Applications of Pure Steam Generators

  • Pharmaceutical Industry: Sterilization of equipment, pipelines, and cleanroom environments.

  • Biotechnology: Used in fermentation processes and sterilization of bioreactors.

  • Healthcare: Surgical instrument sterilization and autoclaving.

  • Food Processing: Used in aseptic packaging and sterilization of food production lines.

Benefits of Using Pure Steam Generators

  • Microbial-free steam production prevents contamination.

  • Compliance with global standards (cGMP, USP, ASME BPE).

  • Reduced risk of endotoxins and particles, ensuring product safety.

  • Energy-efficient designs lower operational costs.

Pure steam generators offer a significant advantage over traditional boiler systems in terms of sterility assurance and operational efficiency. Since the steam produced is entirely free from non-condensable gases and particulate matter, it enhances product safety in pharmaceutical and biotech applications. Additionally, PSG systems reduce the risk of corrosion in steam distribution lines, ensuring longevity and reducing maintenance costs. As sustainability becomes a critical factor in industrial operations, many companies are investing in energy-efficient PSG systems to reduce their carbon footprint.


Thursday, February 20, 2025

Comparing Hot & Cold WFI Generation Systems: Which One is Right for You?

Water for Injection (WFI) is essential for pharmaceutical manufacturing, and selecting the right generation system is crucial for maintaining compliance and efficiency. The two primary methods of WFI generation—hot and cold systems—each have unique advantages and challenges. This article compares both options to help manufacturers determine the most suitable system for their needs.

Understanding Hot WFI Generation

Hot WFI generation utilizes distillation to produce ultra-pure water. Multi-effect distillation (MED) and vapor compression (VC) are common techniques used to generate WFI at high temperatures, typically above 80°C.

Hot and Cold Water for Injection Generation Plant

Advantages of Hot WFI Generation:

  • Superior Microbial Control: High temperatures prevent microbial contamination.

  • Regulatory Compliance: Meets global pharmacopeial standards, including USP and EP.

  • Sterile Storage & Distribution: Heated water reduces biofilm formation in distribution systems.

Challenges of Hot WFI Generation:

  • High Energy Consumption: Distillation processes require significant energy input.

  • Expensive Infrastructure: Requires insulated piping and specialized storage tanks.

  • Regular Maintenance: Scaling and fouling of heat exchangers must be managed.

Understanding Cold WFI Generation

Cold WFI systems use advanced membrane technologies such as reverse osmosis (RO), ultrafiltration (UF), and electrodeionization (EDI) to produce high-purity water at ambient temperatures.

Advantages of Cold WFI Generation:

  • Energy Efficiency: Lower operational costs compared to distillation-based systems.

  • Compact Design: Requires less infrastructure, making it ideal for smaller facilities.

  • Modern Compliance: European Pharmacopoeia (EP) now allows membrane-based WFI generation.

Challenges of Cold WFI Generation:

  • Microbial Growth Risk: Requires stringent sanitization protocols and UV treatment.

  • Complex Monitoring: Real-time microbial and chemical control systems are necessary.

  • Regulatory Variation: Not universally accepted, particularly in certain U.S. regulations.

Key Factors to Consider When Choosing a WFI System

Pharmaceutical manufacturers should evaluate the following factors when selecting a WFI generation system:

  1. Regulatory Requirements: Ensure compliance with USP, EP, and GMP guidelines.

  2. Operational Costs: Compare energy consumption, maintenance, and infrastructure expenses.

  3. Facility Size & Layout: Assess available space and system integration feasibility.

  4. Microbial Control Strategy: Choose a system that aligns with your risk management approach.

  5. Long-Term Sustainability: Consider environmental impact and future regulatory trends.

Conclusion: Making the Right Choice

Both hot and cold WFI generation systems have advantages depending on production needs. Hot WFI systems offer superior microbial control and compliance but have high energy costs. Cold WFI systems provide energy efficiency and modern compliance but require rigorous microbial monitoring. Choosing the right system involves balancing regulatory requirements, operational costs, and facility infrastructure to ensure long-term efficiency and compliance.


Pharma Water System Validation: Critical Parameters, Process & Compliance

In pharmaceutical and biotech laboratories, producing high-purity water is not enough—it must also be proven, documented, and consistently c...